
Performance Proven Before It Leaves Our Facility
From raw materials and manufacturing processes to finished cable performance, Champlain Cable integrates testing and quality assurance throughout production to deliver consistent, reliable wire and cable for demanding applications.
Overview
Tested. Verified. Ready to Perform.
QUALITY THROUGHOUT THE PROCESS
Quality assurance at Champlain Cable goes beyond inspecting the finished product. Our approach integrates quality controls throughout development and manufacturing to help ensure materials, processes, and finished cables consistently meet defined requirements.
Process controls, repeatable manufacturing practices, laboratory testing, and documented quality systems work together to deliver the consistency required for high-performance wire and cable. Champlain describes process repeatability and quality assurance as two of its core competencies.
INTEGRATED TESTING
Our fully integrated test laboratory enables our engineering and quality teams to verify cable performance against demanding electrical, mechanical, thermal, and environmental requirements. The result is more than a cable that meets a drawing—it is a product engineered, manufactured, and validated around the requirements of its application.
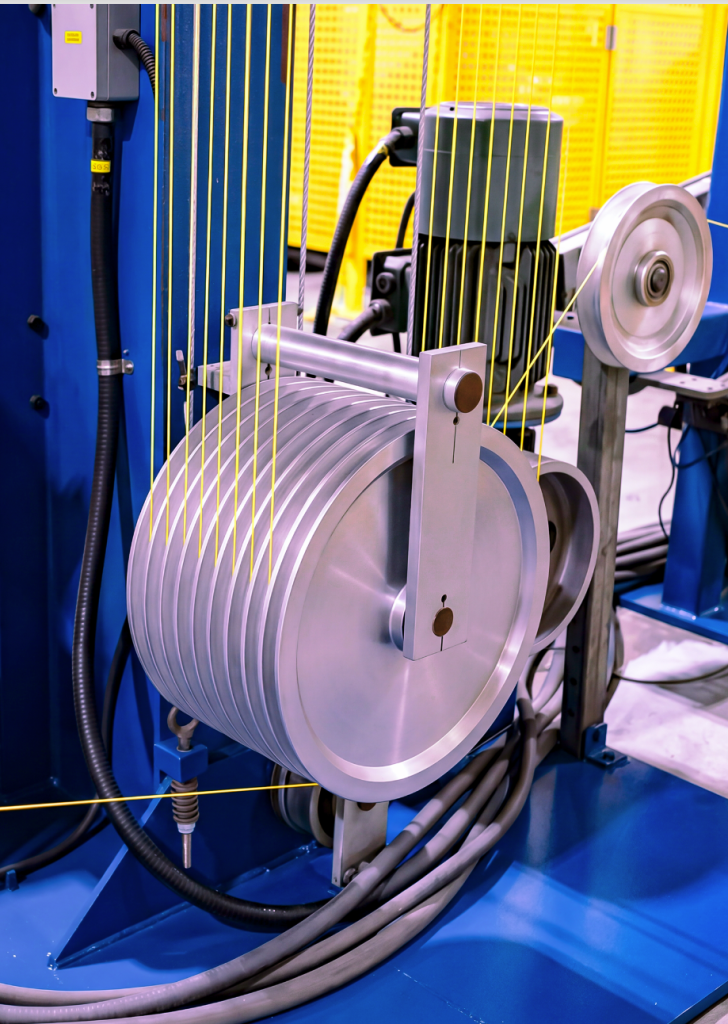
Testing Performance From Every Angle
ELECTRICAL TESTING
Verification of critical electrical characteristics helps ensure cable constructions deliver reliable power and signal performance.
THERMAL TESTING
Cable materials and constructions can be evaluated across demanding temperature conditions to understand both immediate and long-term performance.
MECHANICAL TESTING
Mechanical testing evaluates how materials and finished cable respond to the physical demands encountered during manufacturing, installation, and service.
ENVIRONMENTAL & CHEMICAL TESTING
Cable performance can be evaluated against environmental factors that may degrade conventional materials over time.
CERTIFIED QUALITY
Built on Recognized Quality Systems
Champlain Cable combines technical expertise with documented quality management systems designed to support consistent manufacturing, continuous improvement, and customer-specific requirements. Its current Vermont and Texas certificates cover the design and manufacturing of insulated wire and cable.
AUTOMOTIVE QUALITY MANAGEMENT
QUALITY MANAGEMENT SYSTEM
ADVANCED QUALITY PLANNING
PRODUCTION PART APPROVAL
PROCESS DISCIPLINE
Quality Engineered Into Production
High-performance products require repeatable processes. Champlain’s quality framework uses established methodologies to manage risk, control variation, validate manufacturing processes, and drive continuous improvement. Its supplier quality requirements specifically identify APQP, SPC, FMEA, MSA, and PPAP.
EXAR®
Engineered to withstand extreme temperatures and demanding manufacturing processes while delivering exceptional durability, flexibility, and long-term reliability.
EXRAD®
Field-proven wire and cable solutions designed for automotive and commercial vehicle applications where performance, efficiency, and durability are critical.
DATACLEAR®
High-performance data communication cables built for military, naval, and mission-critical applications where reliability and environmental resistance are essential.
DATARAD®
Advanced lead wire and Ethernet cable solutions engineered for high-temperature automotive and commercial vehicle applications.
Knowledge Center
Learn More About Our Technologies
Explore additional resources covering polymer science, insulation technologies, product innovations, and the engineering expertise behind Champlain Cable’s solutions.
CONTACT US
Let’s Solve Your Next Challenge
Have a question, project, or technical challenge? Let’s start the conversation.